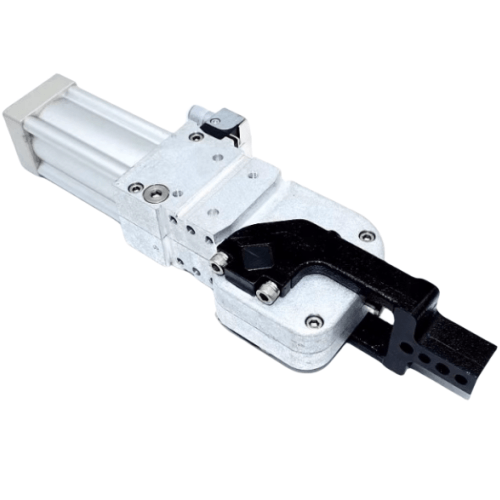
Airtac JCK High Strength Welding Clamping Cylinder JCK40X75KN
Genuine AirTAC welding clamp cylinder, order code JCK40X75KN from the JCK40 range. The options this code selects are decoded below; series data follow the official AirTAC catalog.
- Opening angle75°
- Arm position and clamp armHorizontal arm · No clamp arm
- Sensor and threadNPN electrical sensor (KN) · PT thread
- Bore40 mm
- PortPT1/8
- Output torque (0.5 MPa)120 N·m
- No minimum order. A single piece can be ordered.
- Ready in 3–5 business days. That is the time we take to process the order and hand it to the carrier. Transit time after that depends on the destination.
About the Airtac JCK High Strength Welding Clamping Cylinder JCK40X75KN
With the KN suffix, this JCK40 power clamp reports clamp and open positions through an NPN electrical sensor rated 10 - 30 V DC with a 2 mm sensing distance, matching sinking PLC inputs on automated fixtures. The 40 mm bore and toggle-link mechanism deliver 120 N.m of clamping torque at 0.5 MPa and lock mechanically at up to 380 N.m holding torque if the air supply fails.
The opening angle is fixed at 75 degrees in this order code and the arm position is horizontal, with PT1/8 ports as standard (G-thread bodies exist under the G option). Air cushioning softens both strokes, minimum cycle time is 1 s to clamp and 1 s to open, and no clamp arm is included, so R, C or L layout AM1/AM3 arms or fully custom tooling can be added afterwards.
Airtac JCK High Strength Welding Clamping Cylinder JCK40X75KN Technical Specifications
| Order code | JCK40X75KN |
|---|---|
| Product | Welding Clamp Cylinder |
| Opening angle | 75° |
| Arm position and clamp arm | Horizontal arm · No clamp arm |
| Sensor and thread | NPN electrical sensor (KN) · PT thread |
| Bore | 40 mm |
|---|---|
| Port | PT1/8 |
| Output torque (0.5 MPa) | 120 N·m |
| Maximum holding torque | 380 N·m |
| Maximum load torque | 2.2 N·m (1 s cycle) · 3.3 N·m (2 s cycle) |
| Clamping torque 0.3 / 0.5 / 0.8 MPa | 72 / 120 / 191 N·m |
| Weight (135°, 15 mm arm) | 2.2 kg |
| Acting | Double acting |
| Fluid | Air, filtered to 40 µm |
| Operating pressure | 0.3 - 0.8 MPa (43 - 116 psi) |
| Proof pressure | 1.2 MPa (175 psi) |
| Temperature | -20 to +70 °C |
| Opening angle | 15 - 135° in 15° steps |
| Clamp / open time | 1 s / 1 s minimum |
| Position sensing | Electrical or pneumatic sensor |
| Cushion | Air cushion |
Source: AirTAC JCK series datasheet (p.373-374, p.387), ordering code and specifications.
How to choose
Among the three sensor choices at 75 degrees, JCK40X75KN is the pick for controllers that read NPN sinking signals; choose JCK40X75K for PNP sourcing or JCK40X75KA for a pneumatic signal. All three share identical 40 mm bore mechanics, so the decision is purely the feedback type. If the arm must later swing vertically, the same build exists under the V prefix as JCKV40X75KN, and for wider part-loading clearance step up to neighboring angles such as JCK40X90KN or JCK40X105KN.
Applications
Sinking-input PLC monitoring
The NPN sensor switches at a 2 mm sensing distance, letting weld-cell controllers confirm clamp-done and open-done per station with standard sinking input cards.
Robotic weld end effectors and beds
A 75-degree horizontal swing retracts the clamp clear of the torch path, while the 2.2 N.m (1 s cycle) / 3.3 N.m (2 s cycle) load torque limits guide arm sizing.
Custom tooling on four-face mounting
Since this code omits the clamp arm, fixture builders machine their own levers and bolt them to a body that mounts on four faces with DIN-standard dimensions.
FAQ
What are the key figures of the JCK40X75KN?
Bore 40 mm; opening angle 75 degrees, horizontal arm position; port PT1/8; output torque 120 N.m at 0.5 MPa; maximum holding torque 380 N.m; load torque limit 2.2 N.m at a 1 s cycle, 3.3 N.m at 2 s; operating pressure 0.3 - 0.8 MPa (43 - 116 psi); proof pressure 1.2 MPa (175 psi); temperature -20 to +70 C; minimum clamp and open time 1 s each; air cushion; NPN sensor, 10 - 30 V DC, 2 mm sensing distance; no clamp arm included.
Does the KN sensor require electrical wiring at the clamp?
Yes. KN is an electrical NPN position sensor fed with 10 - 30 V DC and sensing at 2 mm, so a cable runs to each clamp. If you want to avoid wiring in the weld area, order the pneumatic-sensor JCK40X75KA, or the unsensored version with a blank sensor field if the PLC does not need position feedback.