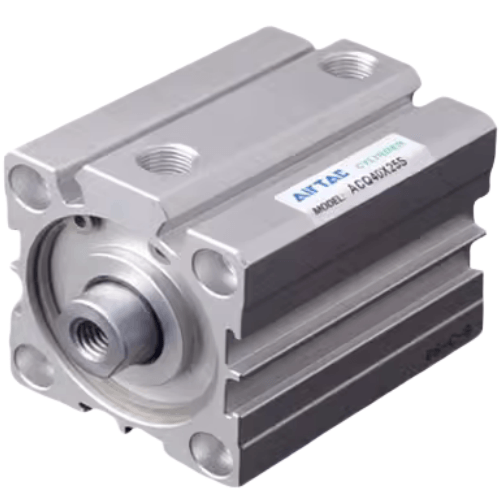
Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S
The AirTAC Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S is a genuine double-acting COMPACT (thin) air cylinder built to JIS dimensions, with a Ø40mm bore and 50mm stroke, PT1/8 air ports and a C-clip / riveted short body that saves mounting depth. Magnetic-switch slots around the body accept position sensors.
- BoreØ40 mm
- Stroke50 mm
- Port sizePT1/8
- Acting typeDouble acting
- Rod threadM8×1.25 (F) / M14×1.5 (B)
- ConfigurationStandard compact
- No minimum order. A single piece can be ordered.
- Ready in 3–5 business days. That is the time we take to process the order and hand it to the carrier. Transit time after that depends on the destination.
About the Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S
The B02-ACQ40X50S is a double-acting, single-rod JIS compact cylinder engineered for welding-line automation. The leading B02- prefix designates this as AirTAC's welding-industry dedicated variant of the base ACQ40X50S, meaning it shares the exact same physical specifications while being targeted at fixturing and robot welding cells. It delivers a robust 628.3 N push force at 0.5 MPa alongside a 527.8 N retract force.
This 40 mm bore unit features a 16 mm piston rod and a PT1/8 port. The short C-clip and riveted body design drastically reduces axial footprint compared to round-body alternatives. Because this configuration includes the S option, it possesses a built-in piston magnet compatible with AirTAC reed or electronic switches via the body's peripheral grooves. End-stopping relies on a fixed NBR elastomer bumper rather than an adjustable air cushion.
Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S Technical Specifications
| Model | Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S |
|---|---|
| Series | ACQ JIS compact (thin) cylinder |
| Bore size | Ø40 mm |
| Stroke | 50 mm |
| Acting type | Double acting |
| Port size | PT1/8 |
| Rod end thread | M8×1.25 female / M14×1.5 male (B) |
| Fluid | Air (filtered by 40µm element) |
|---|---|
| Operating pressure | 0.15 – 1.0 MPa |
| Proof pressure | 1.5 MPa |
| Temperature | -20 to +70 °C |
| Speed range | 30 – 500 mm/s |
| Cushion | Bumper (both ends) |
| Max standard stroke | Up to 100 mm |
Specifications follow the official AirTAC ACQ JIS compact-cylinder datasheet. Confirm against the product label before installation. Port thread: PT (standard); G and NPT available. Rod: female thread (blank) / male thread (B).
Theoretical Output Force (Ø40mm)
| Pressure | Push force | Pull force |
|---|---|---|
| 0.5 MPa | 628 N | 528 N |
| 0.7 MPa | 880 N | — |
| Max (@1.0 MPa) | 128 kgf | |
Actual usable force is lower than theoretical due to friction and back-pressure. Size with a safety margin.
Model Code: Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S
| ACQ | JIS compact (thin) double-acting cylinder series. |
|---|---|
| 40 | Bore size in mm. |
| ×50 | Stroke length in mm. |
| S | Built-in magnet for magnetic-switch position sensing (omit = no magnet). |
| B | Male-thread piston rod (omit = female-thread rod). |
Thread: PT standard (G / NPT available). Related ACQ-family variants: ASQ (single-acting push), ATQ (single-acting pull), ACQD (double rod), ACQJ (adjustable stroke), TACQ (guided / non-rotating).
Where the Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S Is Used
Robot Welding Cell Clamping
Secures mild steel brackets in a robotic MIG welding station, utilizing the 628.3 N extend force to hold parts firmly against locators while the short body saves valuable tooling space.
Spot Welding Gun Actuation
Drives the secondary arm of a spot welding gun on an automotive assembly line, where the 50 mm stroke provides rapid opening and closing for high-cycle production.
Weld Fixture Ejection
Ejects completed tubular frames from a multi-point welding jig, using the 527.8 N retract pull to clear the part before the conveyor advances.
Is the Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S the Right Cylinder?
When sizing this actuator, stepping down to the 32 mm bore yields a 402.1 N push at 0.5 MPa, whereas stepping up to the 50 mm bore provides 981.8 N. This 40 mm option sits comfortably in the middle for medium-duty clamping tasks. To confirm your ordering essentials: specify the 40 mm bore, 50 mm stroke, PT1/8 port, the required S magnet, and the default female M8x1.25 rod-end thread. Note that a plain compact cylinder like this drifts if air pressure is lost or the valve is centered; the fixed bumper only decelerates the piston near stroke end and does not lock the load. For fail-safe holding in a welding fixture, an external rod lock or pilot-operated check valve is required.
Quick checklist
- ✓ Required force at your working pressure
- ✓ Short-body depth vs. a round-body cylinder
- ✓ Port/thread type (PT / G / NPT)
- ✓ Magnet (S) for sensors?
- ✓ Female (blank) or male (B) rod thread
- ✓ Side load — avoid on a compact rod
Installation & Maintenance Notes
- check Use clean air filtered to 40µm or finer.
- check Keep within 0.15 – 1.0 MPa operating pressure.
- check Avoid side load on the short piston rod.
- check Very long strokes are unsuitable for the compact body.
- check Handle the C-clip carefully; seat it fully in its groove.
- check Installation by qualified personnel per AirTAC docs.
Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S FAQ
At 0.5 MPa, the push (extend) force is 628.3 N and the pull (retract) force is 527.8 N. At 0.7 MPa, the push force reaches 879.6 N. The maximum push force is 128 kgf at 1.0 MPa. Operating pressure ranges from 0.15-1.0 MPa, with a speed of 30-500 mm/s.
The B02- prefix indicates this is the welding-industry dedicated version of the ACQ40X50S, mechanically identical to the base model. It does not have adjustable air cushions; instead, it uses a fixed NBR elastomer bumper at each end to absorb the stop. For high-energy welding automation cycles, consider adding an external shock absorber.
Authorized Export Seller
Genuine AirTAC parts produced by AirTAC factory.
1-Year Warranty
Covers non-human-caused product damage.
Fast Dispatch
Standard models are processed and dispatched in 3-5 business days.
Fast Reply
Most inquiries answered within 7-8 hours.
Request a Quote for Airtac B02-ACQ Ultra-Thin Welding Special Cylinder B02-ACQ40X50S
Send us the quantity and destination. We confirm price, stock and lead time — usually within 7-8 hours.