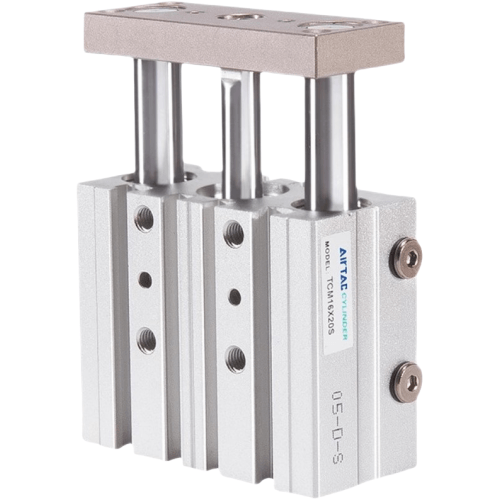
Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S
The AirTAC Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S is a genuine JIS-standard guided cylinder with a Ø32mm bore and 100mm stroke on twin guide rods. Its integrated brass sliding bearing gives high radial-load and impact resistance — about double the horizontal impact tolerance of a plain cylinder, holding the tool square to ±0.06° of rotation without any external linear guide.
- BoreØ32 mm
- Stroke100 mm
- Port size1/8"
- BearingBrass sliding bearing
- Non-rotating±0.06°
- CushionRubber bumper
- No minimum order. A single piece can be ordered.
- Ready in 3–5 business days. That is the time we take to process the order and hand it to the carrier. Transit time after that depends on the destination.
About the Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S
The AirTAC B02-TCM32X100S is a JIS guided twin-rod cylinder built for welding-line automation. The B02- prefix marks this as a welding-industry dedicated variant of the base TCM32X100S, meaning it is mechanically identical to the standard model but targeted at clamping and fixturing tasks in robotic weld cells. As a double-acting drive unit, it generates 402 N of push at 0.5 MPa through its Ø16 mm piston rod.
The integrated brass sliding bearing handles radial loads and hard impacts, shrugging off grit and weld spatter where a steel-ball guide would jam. It delivers a tight ±0.06° non-rotating tolerance, keeping a clamping arm square under off-centre loads. Stroke ends are damped by fixed elastomer pads rather than an adjustable cushion. Air feeds via 1/8" ports, and the standard built-in magnet works with CS1 reed or DS1 electronic switches in the four body slots.
Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S Technical Specifications
| Model | Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S |
|---|---|
| Series | TCM JIS guided (twin-rod) cylinder |
| Bore size | Ø32 mm |
| Stroke | 100 mm |
| Acting type | Double acting |
| Bearing | Brass sliding bearing |
| Port size | 1/8" |
| Fluid | Air (filtered by 40µm element) |
|---|---|
| Operating pressure | 0.15 – 1.0 MPa |
| Proof pressure | 1.5 MPa |
| Temperature | -20 to +70 °C |
| Speed range | 30 – 500 mm/s |
| Non-rotating tolerance | ±0.06° (retracted) |
| Cushion | Rubber bumper |
| Max std stroke | Up to 250 mm |
Specifications follow the official AirTAC TCL/TCM series datasheet (JIS standard). Confirm against the product label before installation. Thread options: PT (blank) / G / NPT. Every TC model ships with a built-in magnet for sensor switches.
Theoretical Output Force (Ø32mm)
| Pressure | Push force | Pull force |
|---|---|---|
| 0.5 MPa | 402 N | 302 N |
| 0.7 MPa | 563 N | — |
| Max | 82 kgf | |
Force is set by the bore and piston rod (Ø16 mm); the twin guide rods carry side load and torque, not thrust. Actual usable force is lower than theoretical due to friction and back-pressure.
Model Code: Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S
| TC | Tri-rod (guided, twin-rod) cylinder, double acting. |
|---|---|
| M | Bearing: Brass sliding bearing (M = brass sliding). |
| 32 | Bore size in mm. |
| ×100 | Stroke length in mm. |
| S | Built-in magnet (standard on TC) for a magnetic sensor switch. |
Sister type: TCL32X100 (steel-ball linear bearing, lower friction & higher precision). Thread codes: blank = PT · G · T = NPT.
Where the Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S Is Used
Spot Welding Clamp
Drives an off-centre clamping arm in a robotic spot weld cell. The brass sliding bearing tolerates weld spatter and grit, delivering 402 N of push while maintaining a ±0.06° non-rotating accuracy.
Weld Fixture Locator
Positions a locating pin for heavy steel plates before the torch fires. The twin guide rods absorb the side load of plate insertion without needing an external linear rail.
Transfer Line Gate
Acts as a heavy stop gate on a weldment transfer line. The impact-tolerant brass bearing shrugs off the shock of arriving pallets, handling the 563 N peak force at 0.7 MPa.
Is the Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S the Right Cylinder?
This Ø32 bore provides 402 N of thrust at 0.5 MPa. If you need less clamping force, step down to the Ø25 bore which yields roughly 245 N. For heavier fixturing, the Ø40 bore offers about 628 N of push. When replacing this unit, match the 32 mm bore, 100 mm stroke, 1/8" port, PT thread form, and the standard S magnet.
Choose the sister TCL series with its steel-ball linear bearing instead if your weld cell demands ultra-low friction or high-precision vertical lifting. Note that this guided cylinder does not hold its load if air pressure is lost or the valve is centred; the rod will drift. Install an external rod lock or pilot check valve for fail-safe clamping.
Quick checklist
- ✓ Required force at your working pressure
- ✓ Side load / torque the guide must carry
- ✓ TCL (precision, low friction) vs TCM (impact, radial load)
- ✓ Stroke & mounting face (top / bottom / rear)
- ✓ Port/thread type (PT/NPT/G)
Installation & Maintenance Notes
- check Use clean air filtered to 40µm or finer.
- check Keep within 0.15 – 1.0 MPa operating pressure.
- check The guide unit takes side load & torque — but do not exceed the max safe load/torque for your stroke.
- check Mount from the top, bottom (screw or T-slot) or rear face; use the precision locating holes.
- check Do not disassemble the fixing block or guide unit — factory-set precision.
- check Fit CS1 / DS1 magnetic switches in the four sensor slots as needed.
Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S FAQ
At 0.5 MPa this 32 mm bore cylinder provides 402 N of push and 302 N of pull. At 0.7 MPa the push increases to 563 N. The theoretical maximum force is 82 kgf.
The B02- prefix designates this as AirTAC's welding-industry dedicated variant of the TCM32X100S; mechanically, the specs are identical to the base model. Each end lands on a fixed TPU bumper to soften the stop, but there is no air-cushion screw to set or adjust.
Authorized Export Seller
Genuine AirTAC parts produced by AirTAC factory.
1-Year Warranty
Covers non-human-caused product damage.
Fast Dispatch
Standard models are processed and dispatched in 3-5 business days.
Fast Reply
Most inquiries answered within 7-8 hours.
Related AirTAC TCM Cylinders
Request a Quote for Airtac B02-TCM Welding Dedicated Triple-Axis Cylinder B02-TCM32X100S
Send us the quantity and destination. We confirm price, stock and lead time — usually within 7-8 hours.